Cost
More material and another print can eat into the margin on every part.
Large-format extrusion 3D printing
Poor layer adhesion can turn a promising print into extra weight, rework and another missed deadline.
Better layer bonds are a production question. LEAM helps you build stronger layer bonds in large-format extrusion 3D printing. We apply heat where the next layer meets the part, giving you more control over bonding and part stability.
01 / Beyond the strength test
A thicker wall here, a slower build there, another round of tests. The workarounds for weak layer bonds can quietly become part of your production cost.
More material and another print can eat into the margin on every part.
Thicker walls and extra reinforcement can add weight beyond the original design.
Every redesign or reprint can push the finished part further down the schedule.
Inconsistent bonds can mean more checks before you can trust the finished part.
Look at the material, time and rework your current process needs. The opportunity is different for every part. We’ll help you work out where stronger bonding could be worth the investment.
02 / How LEAM helps
Good layer adhesion needs heat in the right place.
If the previous layer has cooled too far, the next bead struggles to bond. Keep too much heat in the part, and it can sag or lose its shape. Large-format printing has to manage both.
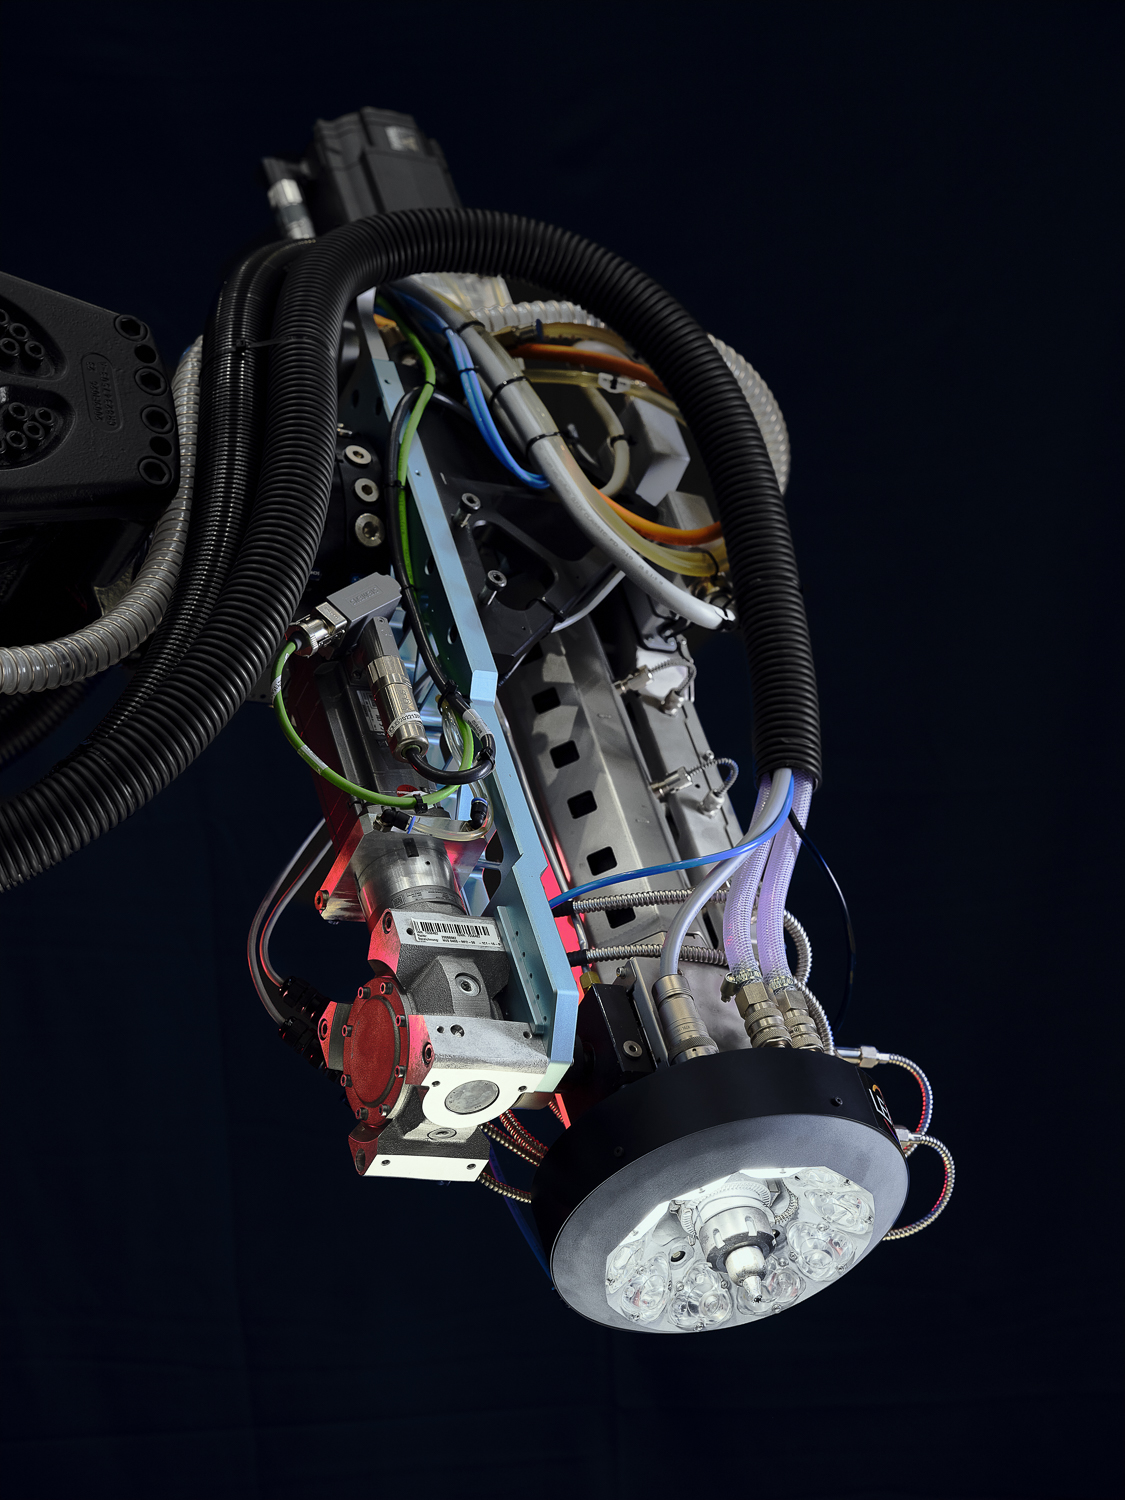
We focus thermal control on the deposition interface, where the new layer meets the printed surface. That helps you improve interlayer bonding while managing the heat that affects the rest of the part.
How LEAM improves layer adhesion ↗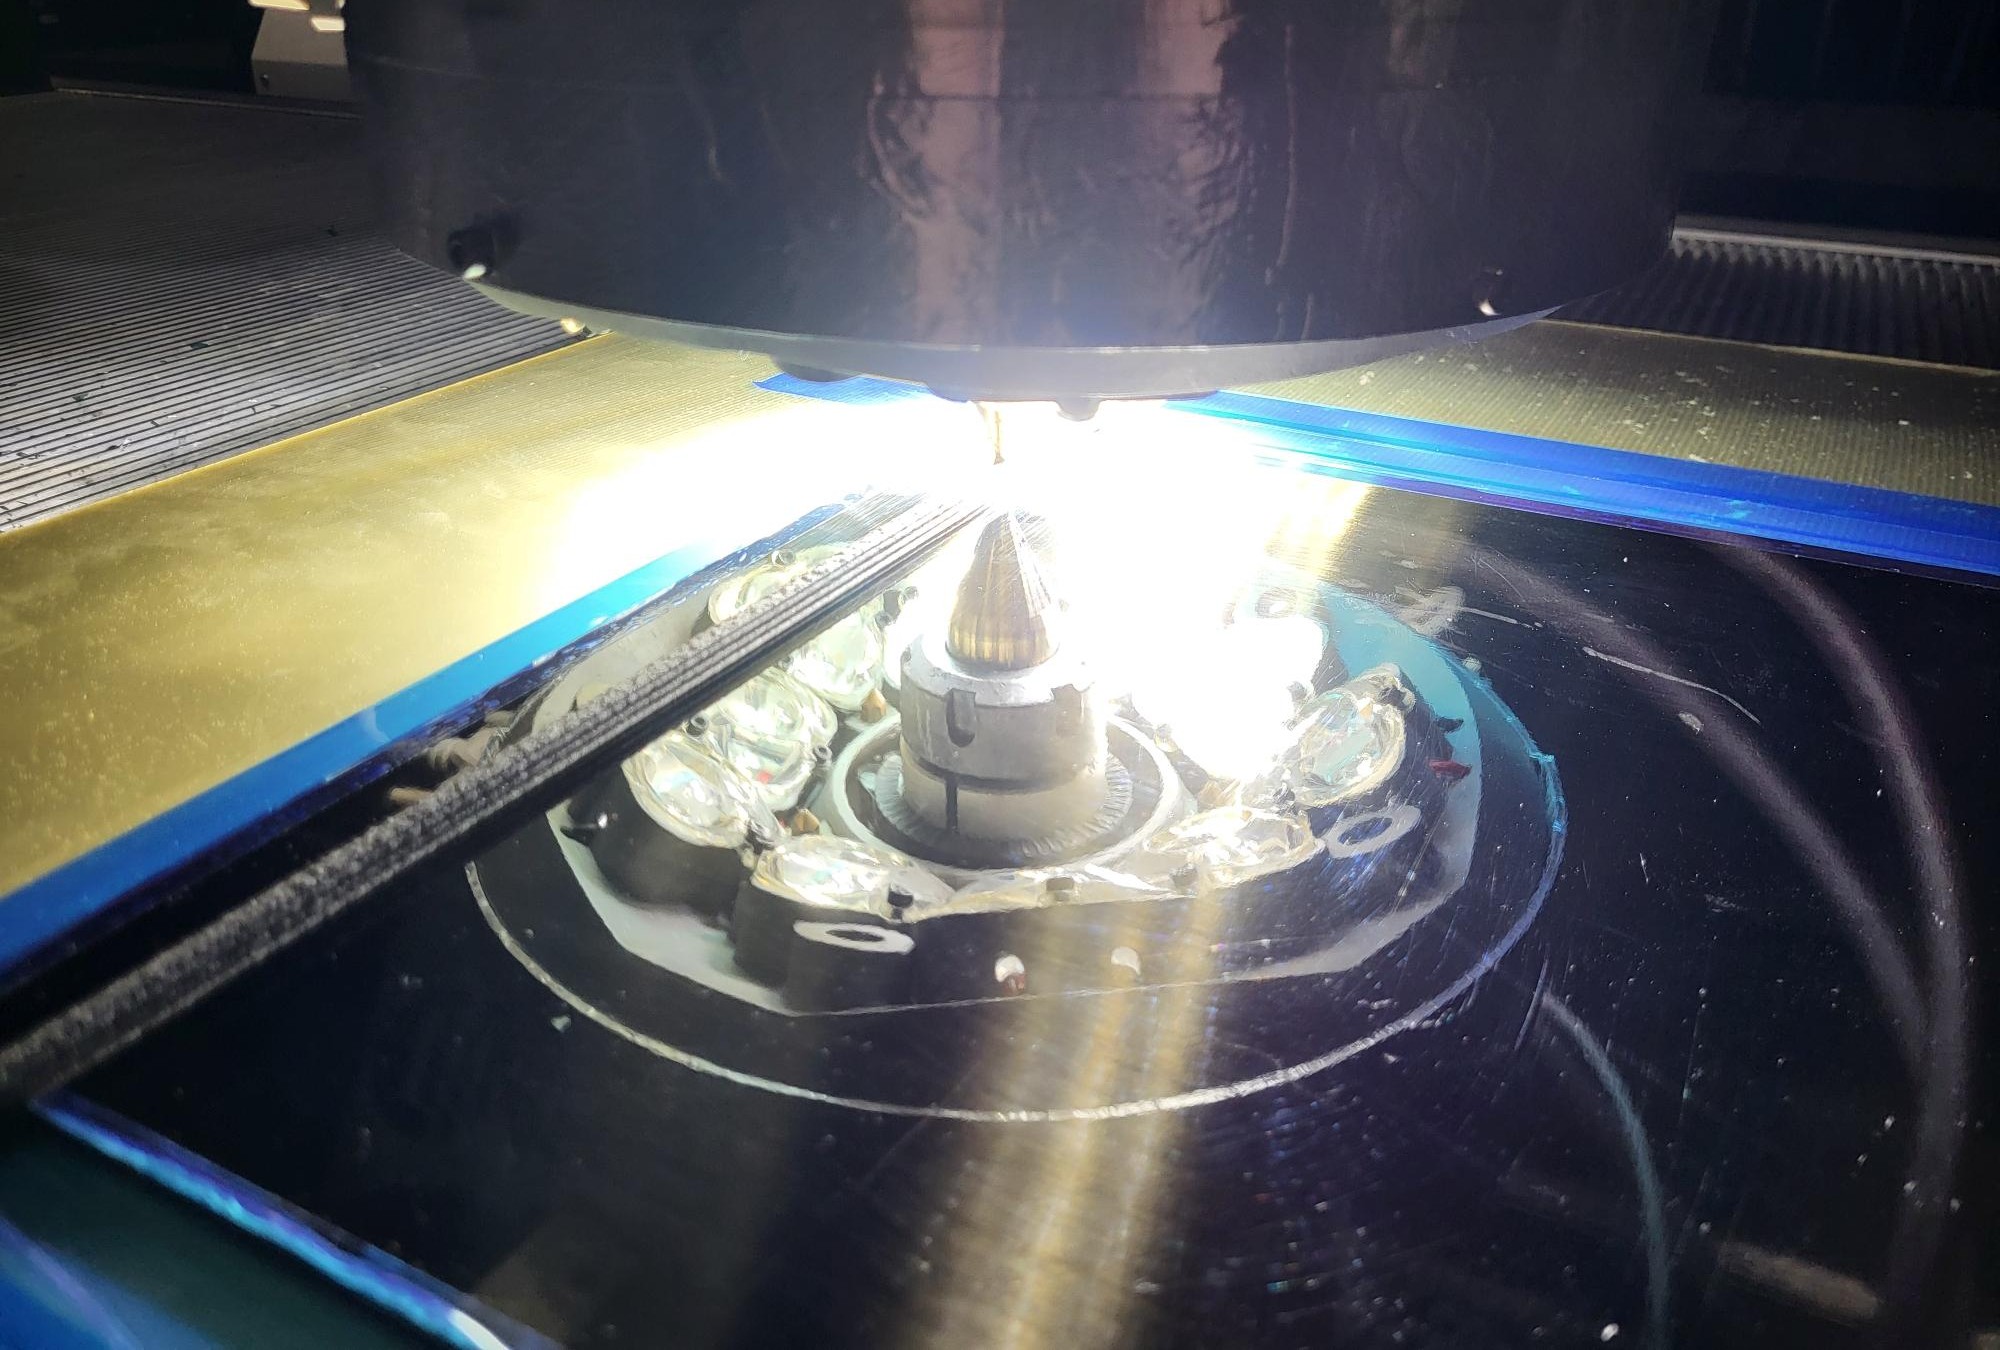
03 / What the tests show
Large-format extrusion AM parts can show 50–75% lower mechanical performance in Z than in X/Y. In other words, the direction across the layers can be much weaker than the directions along them. This compares printed directions, not printed parts with bulk material.
Published LMPAEK trials
Z-direction ultimate tensile strength in unreinforced LMPAEK.
Programmed layer temperature: 300 → 340 °C.
Z-direction ultimate tensile strength in reinforced LMPAEK.
Uncontrolled printing → programmed 340 °C.
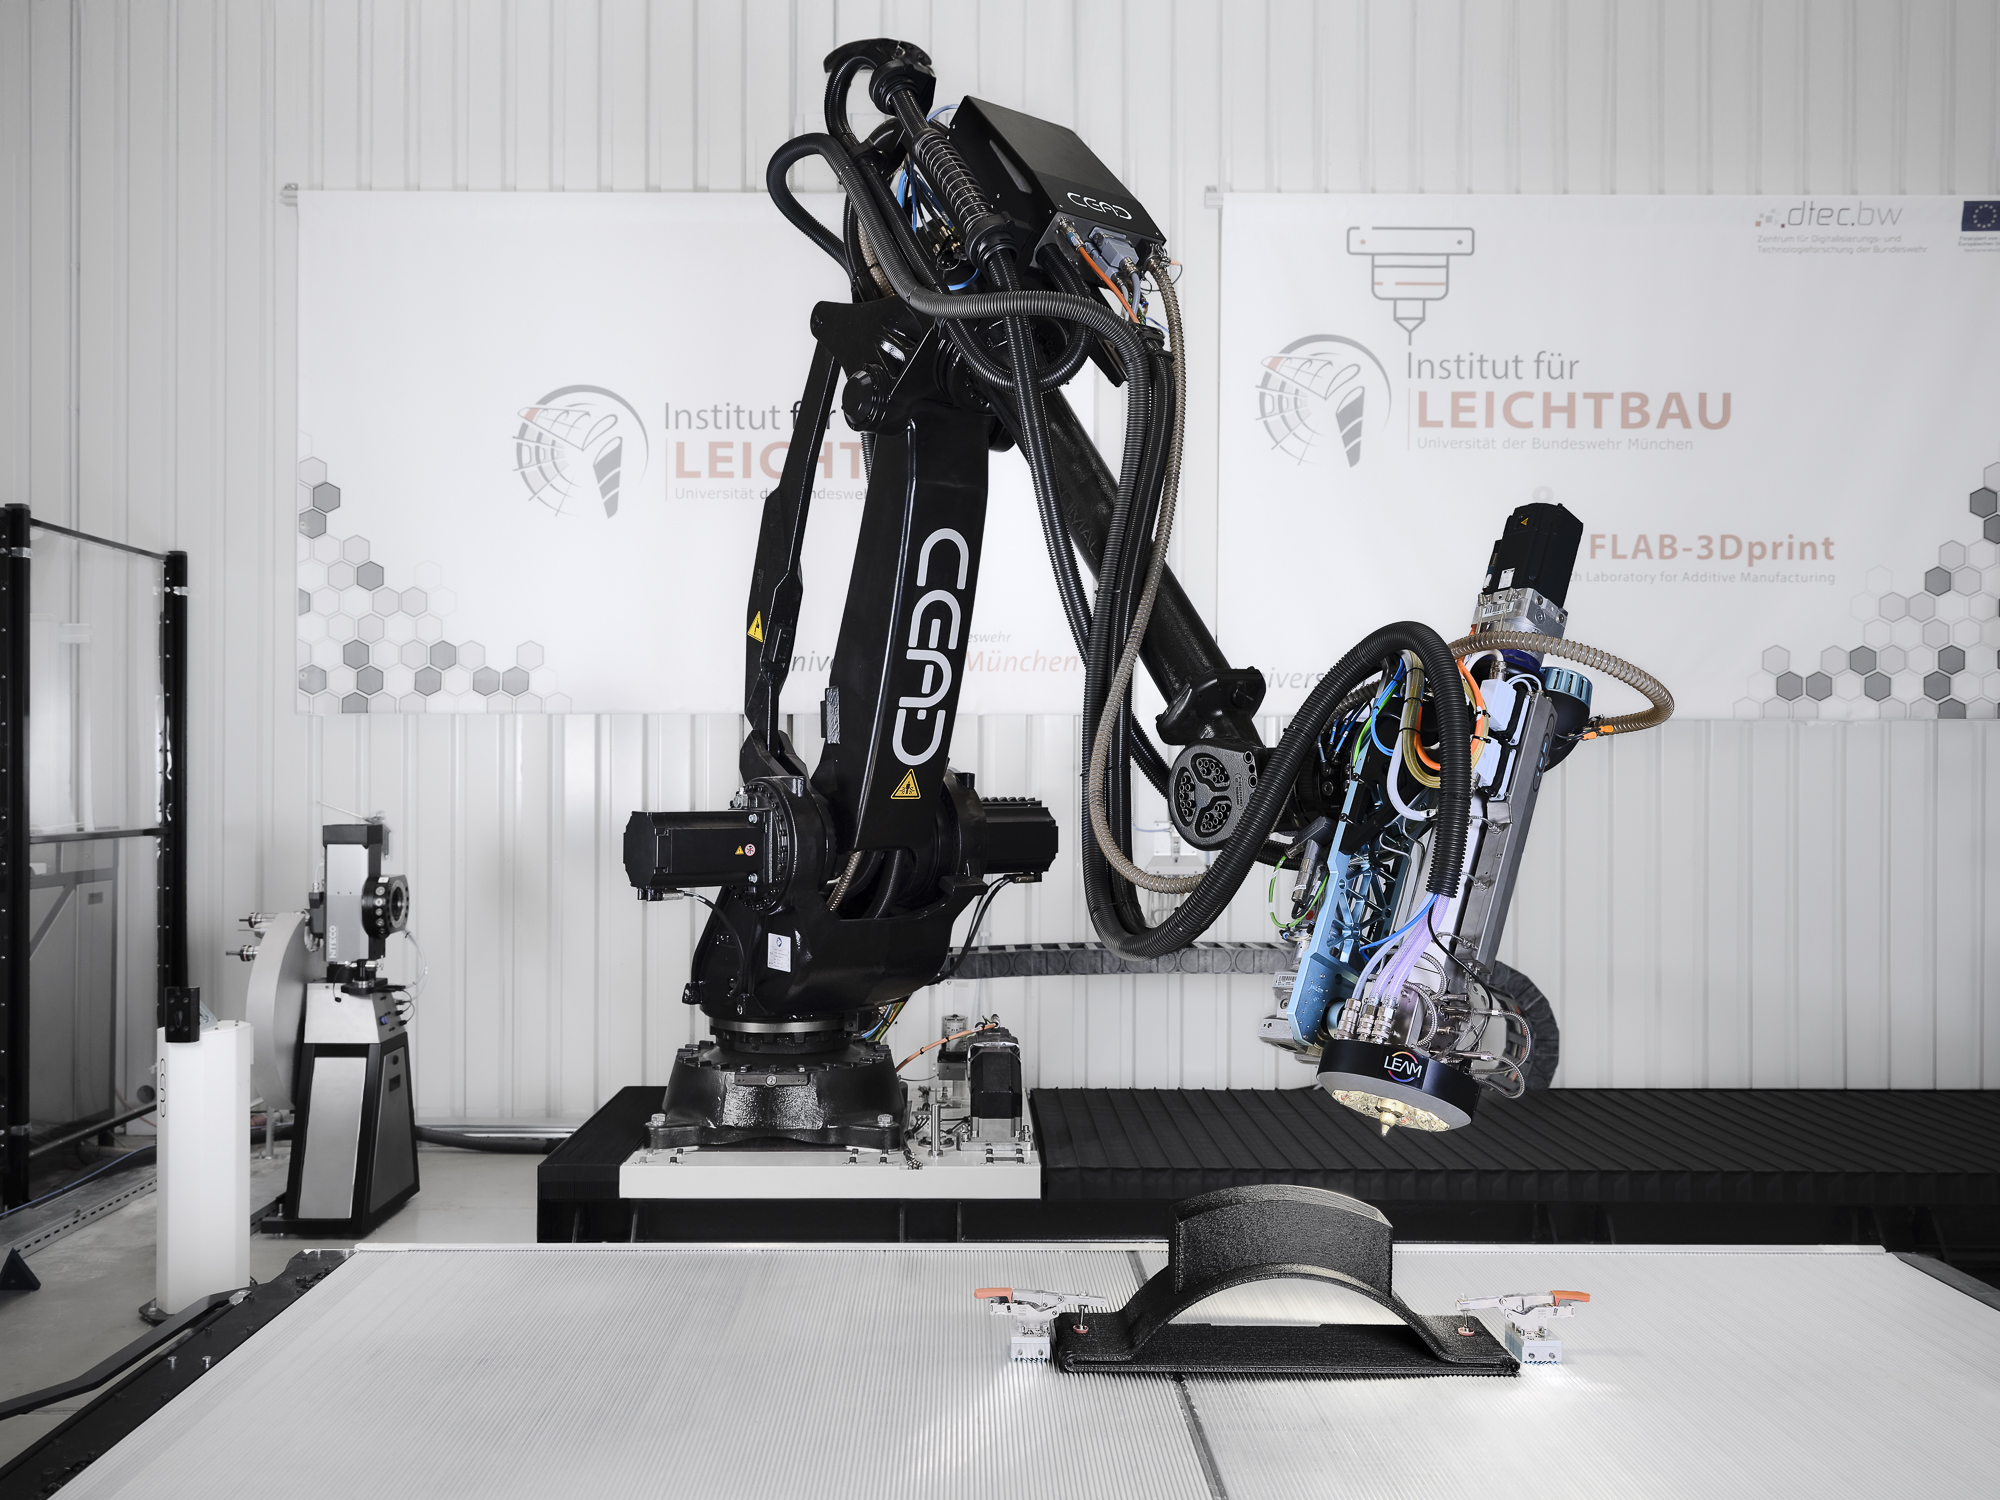
The retrofit system / DEMEX
Bring LEAM thermal control to the extrusion AM platform you already use.
DEMEX is designed for existing extrusion AM platforms. We’ll work through your material, machine and print geometry with you to see how localized thermal control could fit your process.
What are you printing?
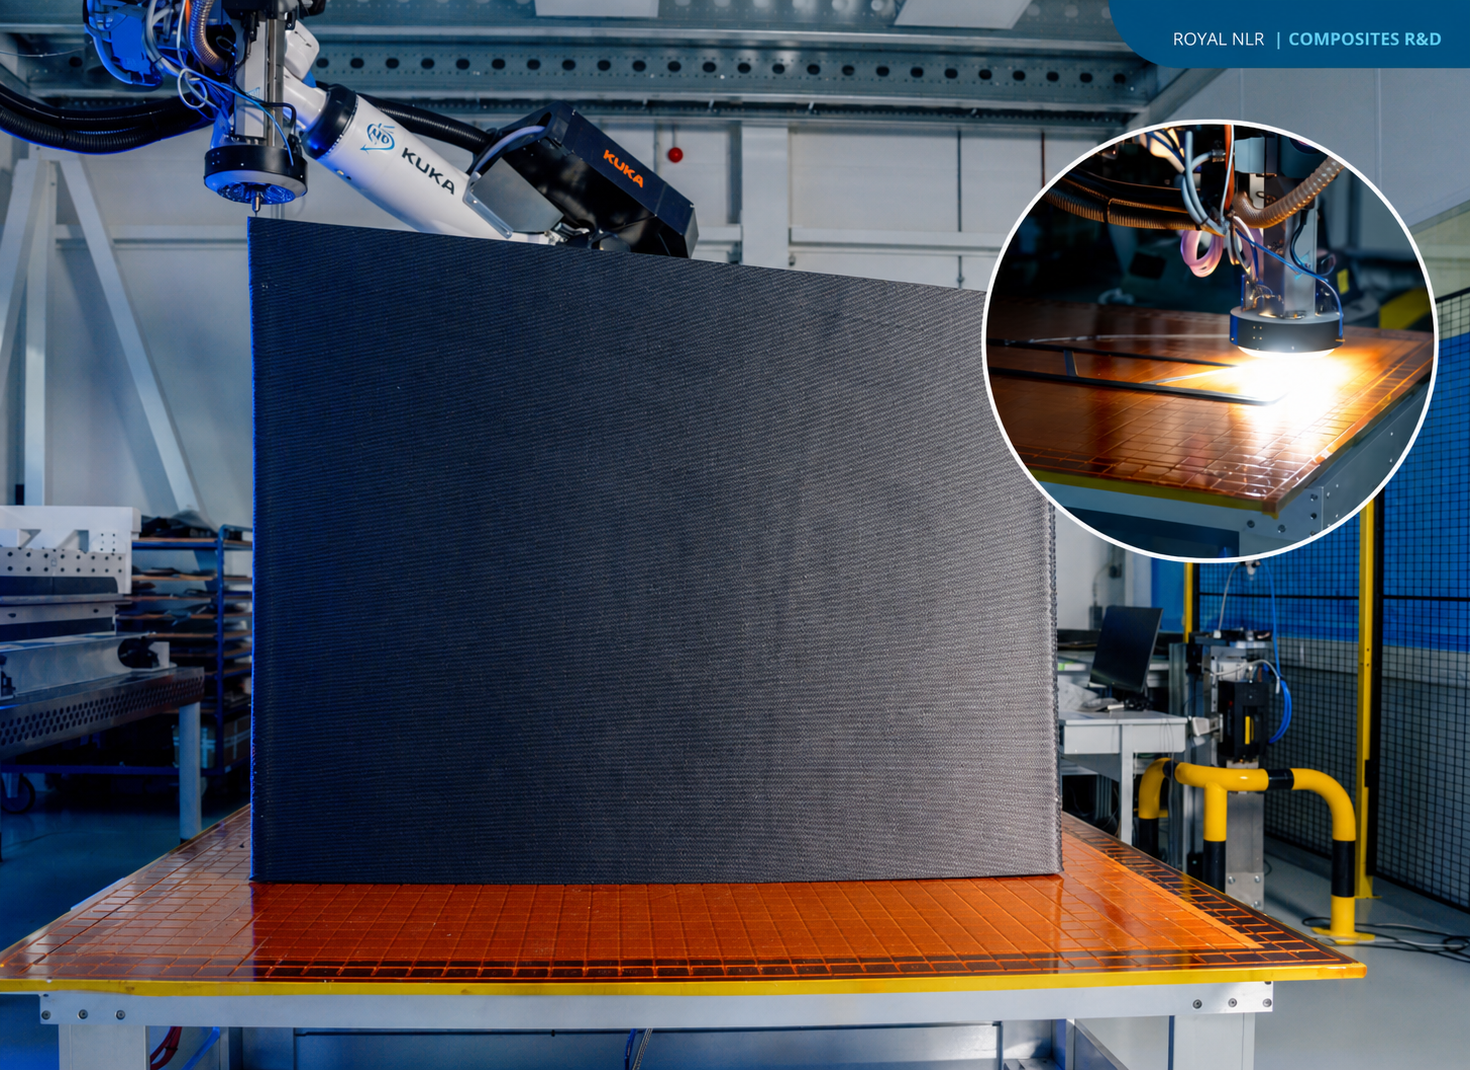
Large printed structures bring layer bonding, weight and build time into the same conversation.
02The right polymer is only the start. The printed part still has to meet the demands of its job.
03A tool earns its place in production when it holds its shape and does the job it was made for.
Find your application ↗From research to the factory floor
These funding, incubation and engineering programs have supported LEAM along the way.
Let’s talk about your part
Tell us what you’re printing and where it falls short. We’ll help you decide whether thermal control could make the difference.